Cutting metal efficiently takes the right tool, and not every laser is up to it. Three types of laser show up most often: CO₂, Nd:YAG and fiber. This article compares them and explains why fiber is the usual choice for metal today.
Why the right laser matters
Metal cutting is common in construction, automotive and manufacturing. The wrong laser means wasted material, slower production and costly upkeep. The right one gives you fast cutting, clean edges, little waste and efficient energy use.
The three types
1. CO₂ lasers
CO₂ lasers are among the oldest and most established types. They generate the beam in a gas mixture, mainly carbon dioxide. They are best on nonmetals such as wood, acrylic and leather, and they cost less to buy than fiber lasers. On metal, they tend to be slower and struggle with reflective metals such as brass and copper. They also need more maintenance because of mirrors and other optics. A CO₂ laser is a sensible choice if you mainly cut nonmetals.
2. Nd:YAG lasers
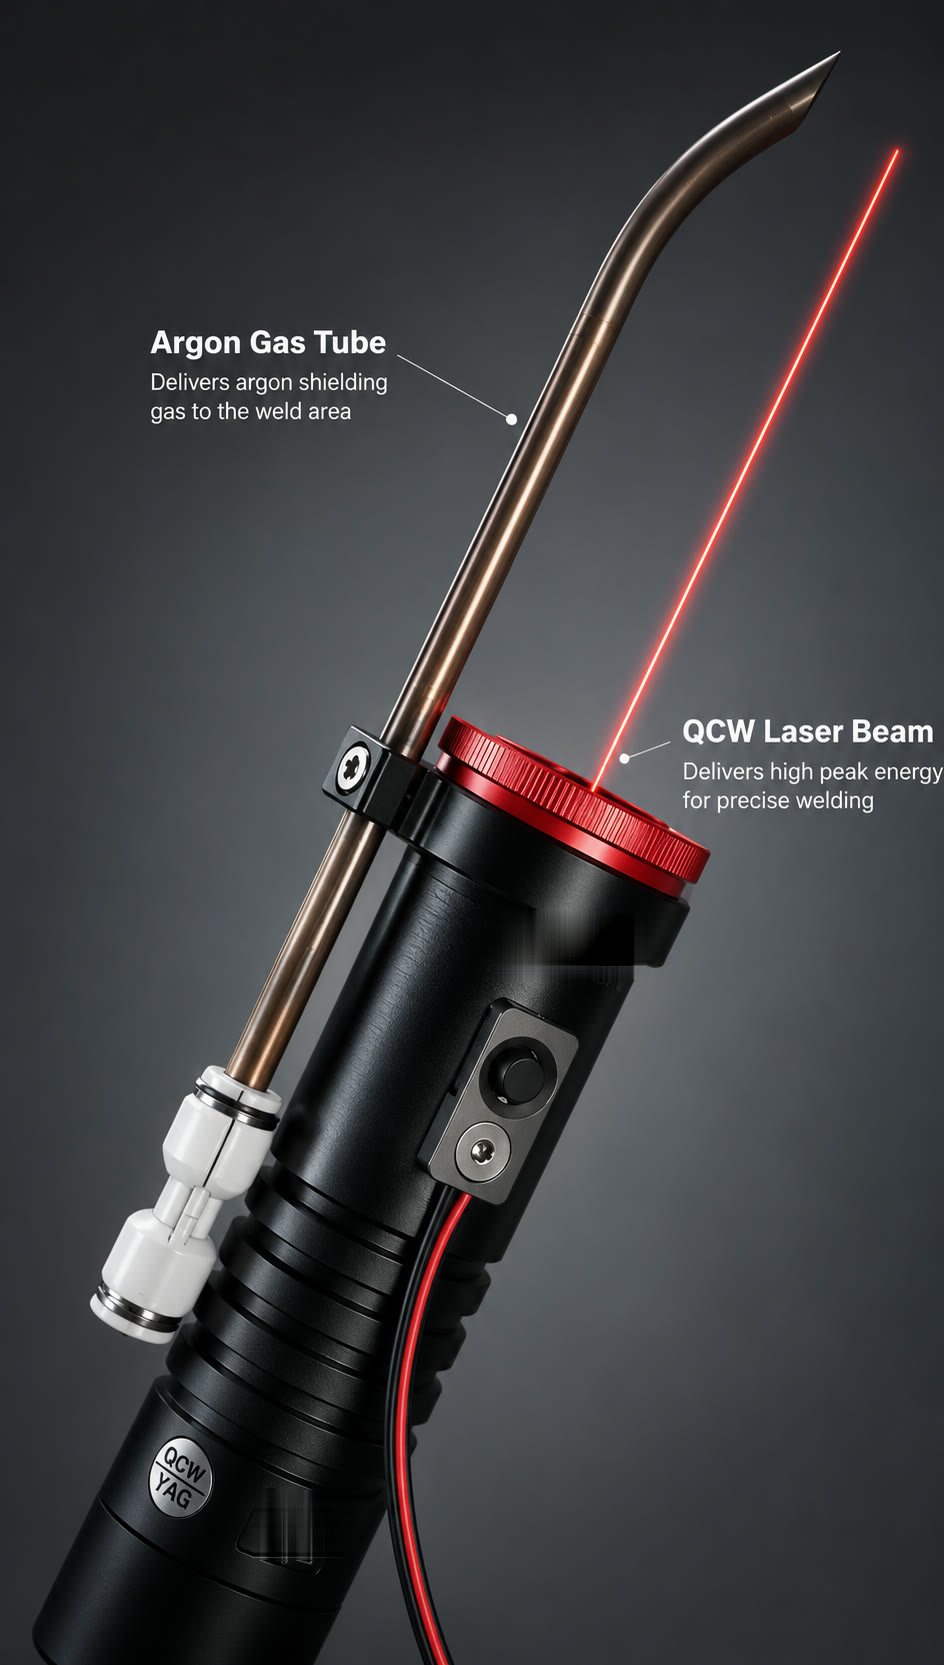
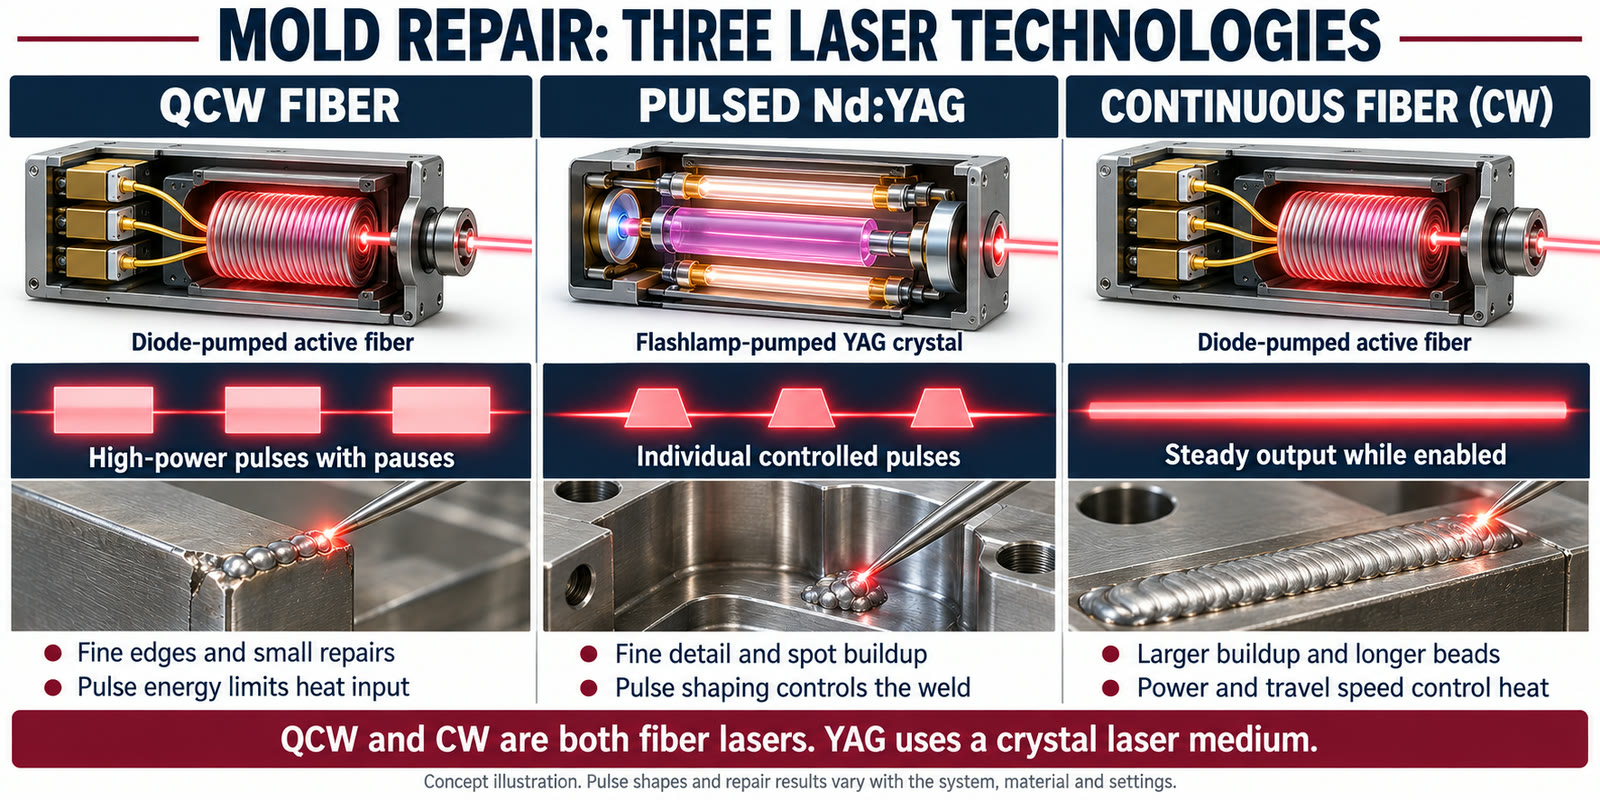
Nd:YAG lasers use a crystal as the laser medium. They are used for deep cuts, for welding and for precision work, and they have a long history in industry. They use more energy than other types and need more maintenance, because of components such as flash lamps. For standard metal cutting, other options are usually more efficient. Ascent uses pulsed Nd:YAG in its mold repair welder, where its short pulses suit rebuilding edges and small defects.
3. Fiber lasers
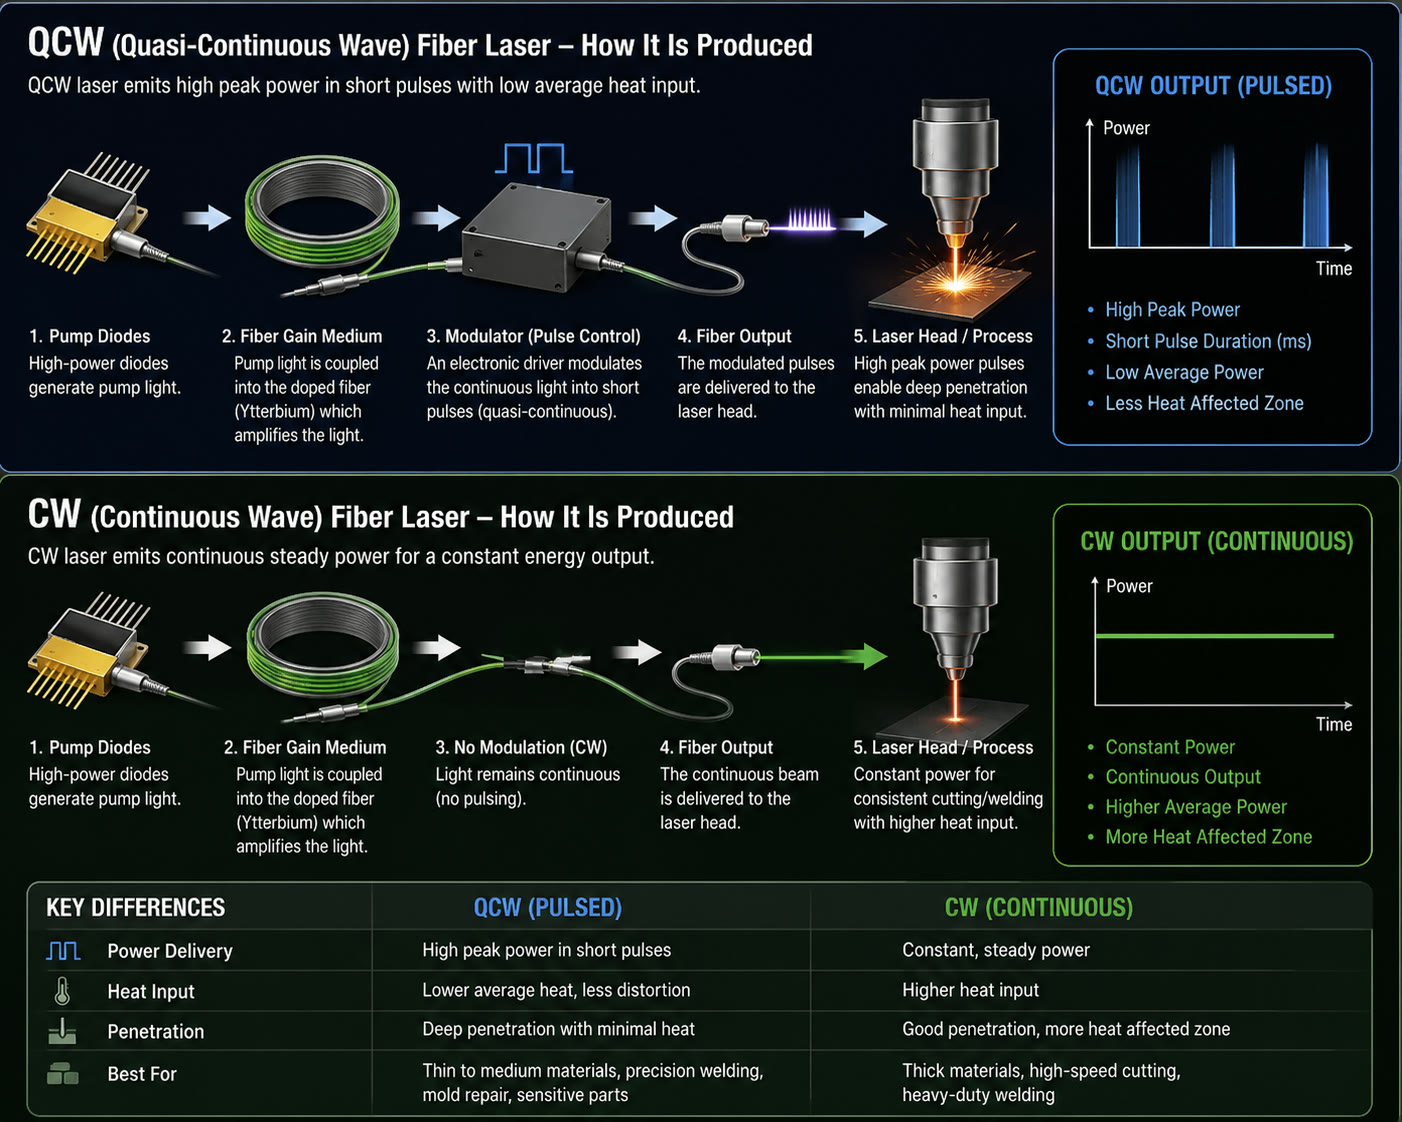
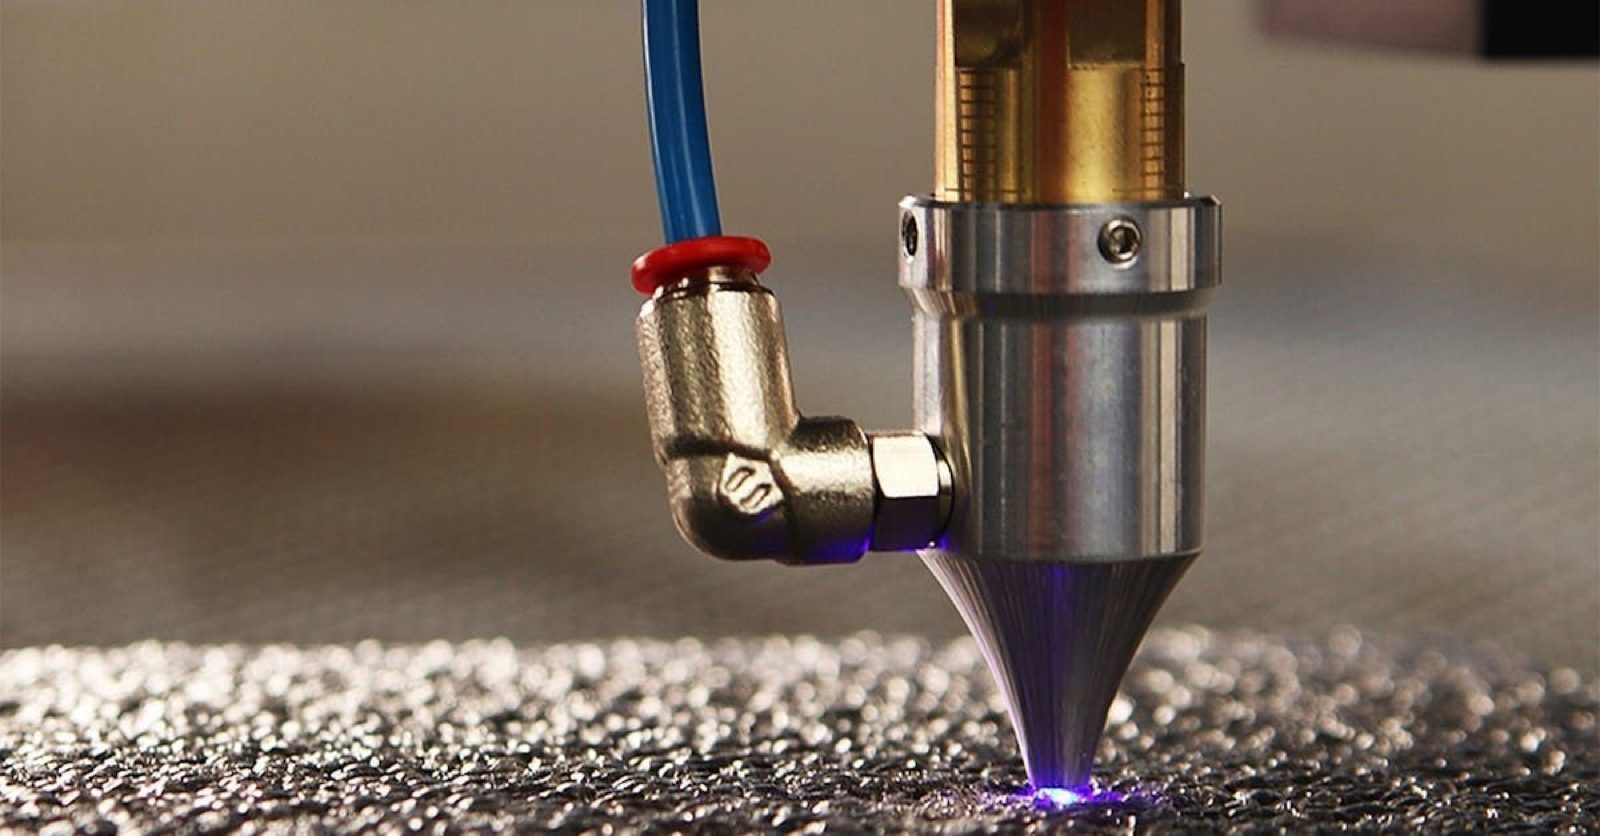
A fiber laser generates and delivers its beam through optical fiber. It cuts stainless steel, carbon steel, aluminum and brass well, and it handles reflective metals that CO₂ lasers struggle with. It cuts thin and medium sheet faster than a CO₂ laser, needs less maintenance because it has a simpler design, and uses less energy. It costs more up front, but the performance and lower running cost make it a practical choice for frequent metal cutting.
Why fiber is best for metal
- Speed. It is considerably faster than CO₂ on thin to medium metal.
- Less maintenance. The beam travels in fiber, not through mirrors.
- Energy. It uses less power.
- Reflective metals. Metals like brass, copper and aluminum reflect CO₂ light and cause problems. A fiber laser handles them with the right settings.
The Ascent fiber laser cutter comes with a 3000W or 4000W source, and its table lists the maximum thickness for carbon steel, stainless steel, brass and aluminum.
Choosing a laser for your work
- Thickness. The product page's cutting table shows what each power can cut.
- Speed. For higher output on metal, choose fiber.
- Budget. CO₂ costs less up front, and fiber costs less to run.
- Material type. For reflective metals, choose fiber.
- Space. Check the footprint of the machine and its support equipment, including the chiller.
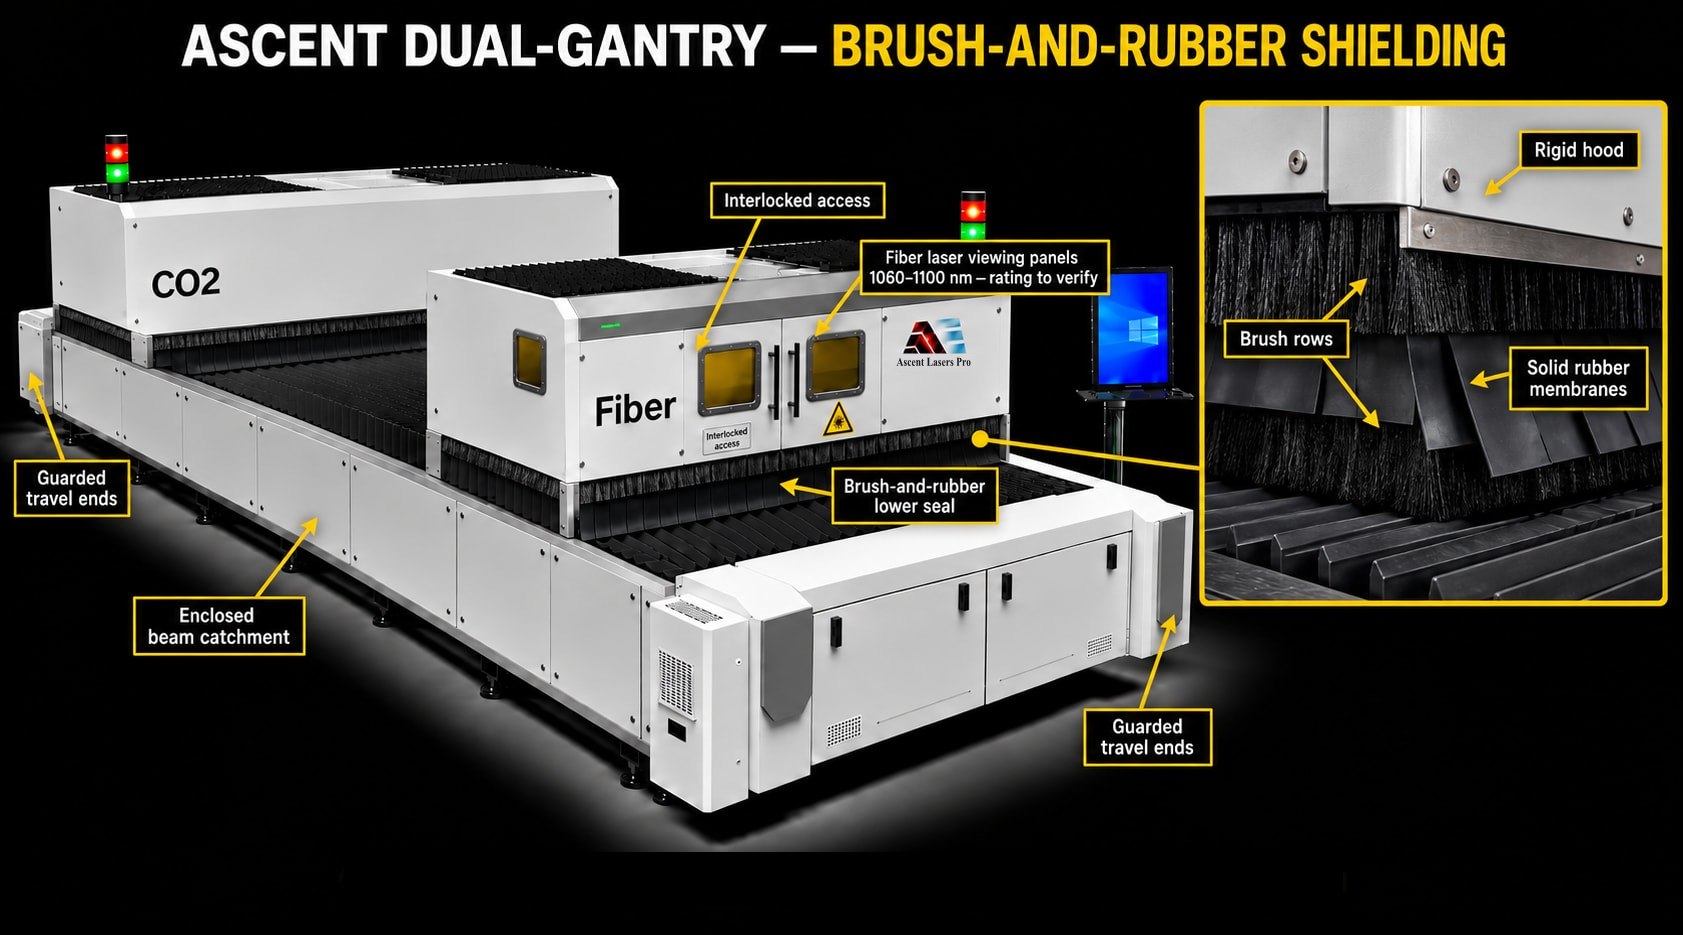
If you cut both metal and nonmetals, consider a combination machine such as the Ascent dual gantry CO₂ and fiber cutter.
Industries
- Construction. Beams, panels and fittings.
- Automotive. Car parts and body structures.
- Electronics. Precise metal components.
- Jewelry. Detailed metal designs.
- Manufacturing. Mass production of metal parts.
Maintaining a fiber laser cutter
- Clean the lens and protective glass regularly.
- Inspect the fiber optic cable for wear.
- Keep the cooling system clean.
- Follow the maker's service schedule.
See our maintenance tips for a CNC laser cutter.
Ascent Lasers Pro fiber laser cutters
The Ascent fiber laser cutter has an autofocus head, a shuttle table and a full enclosure. Installation and operator training at your facility are included in the price, and the cutter has a 1-year warranty on workmanship and non-consumable parts. Contact Ascent Lasers Pro to talk about your metal cutting.