Dual Gantry Laser Cutter: 300W to 600W CO2 and 3000W or 6000W Fiber
A fiber gantry for metals and a CO2 gantry for acrylic, wood and other non-metals
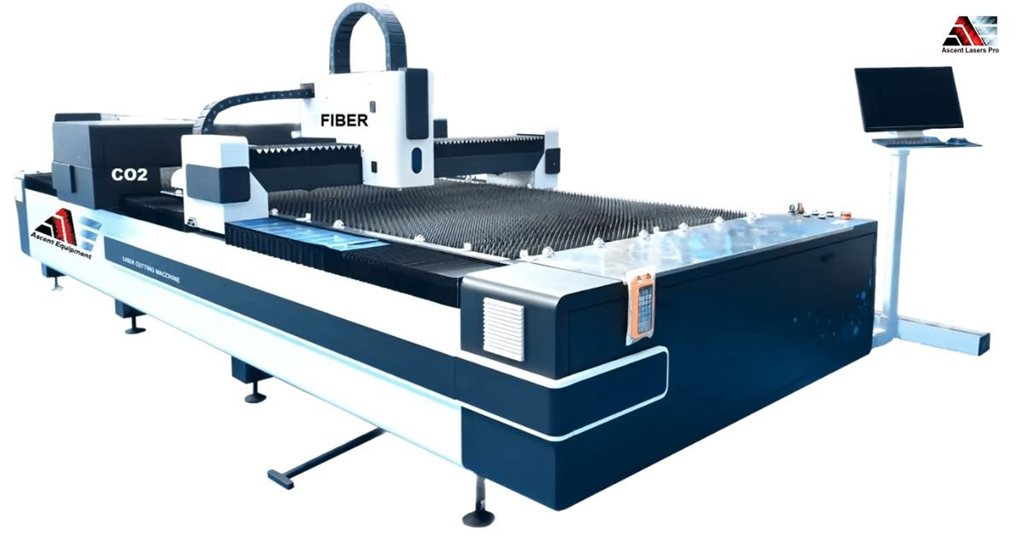
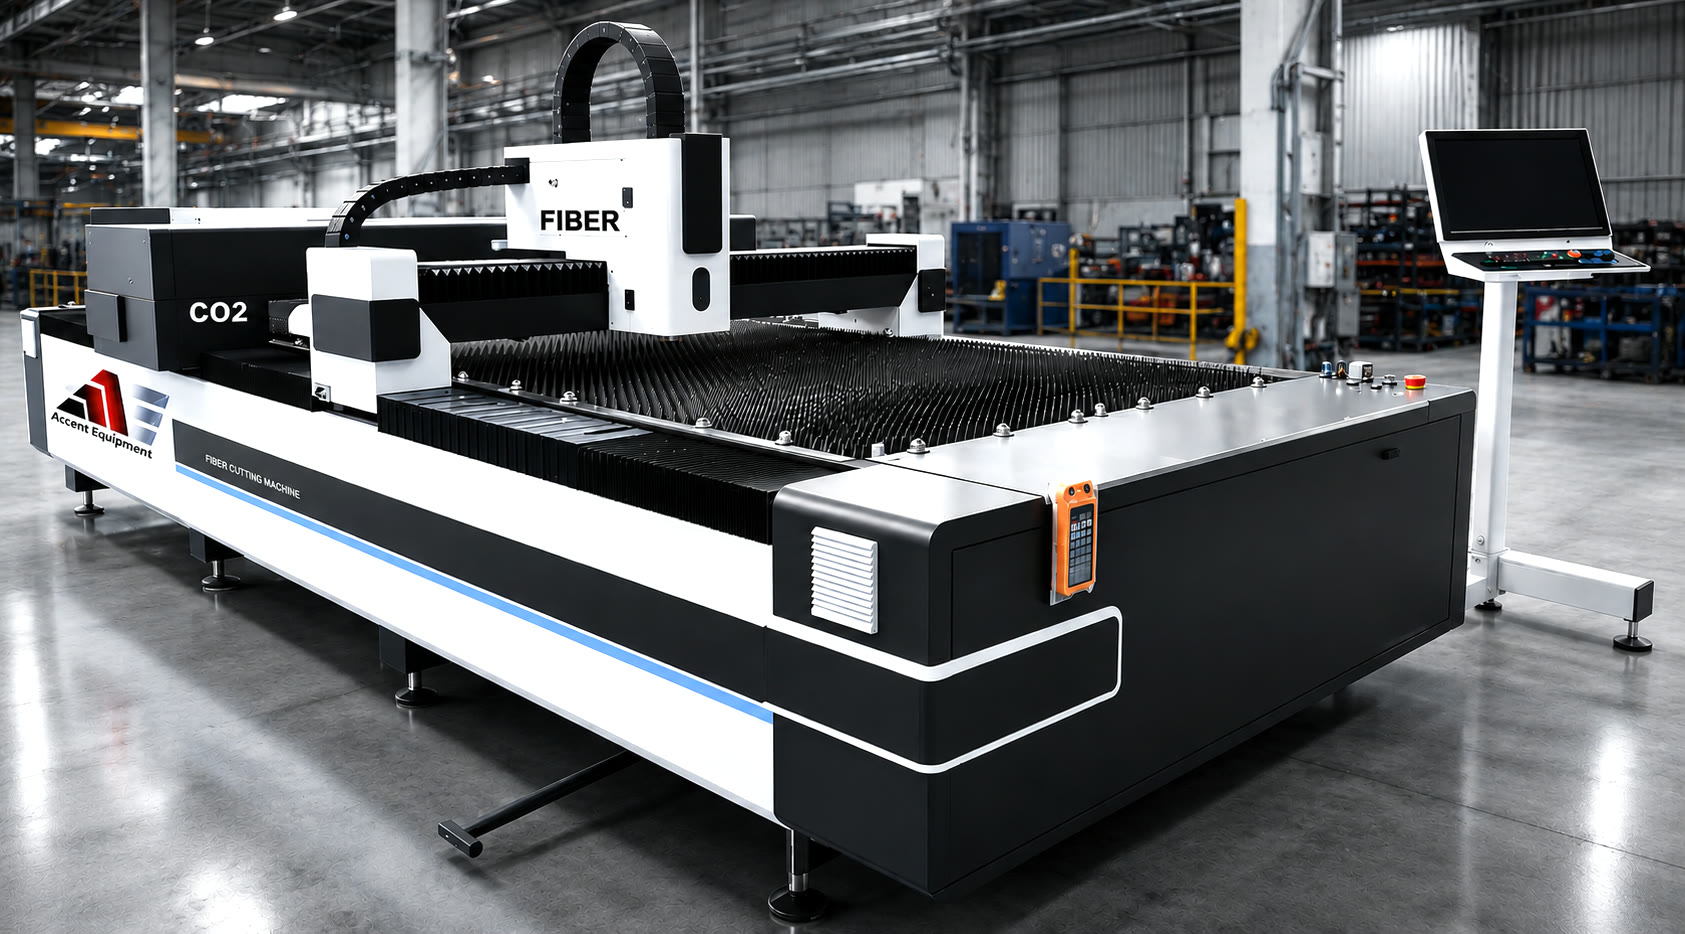
One table, a CO2 gantry and a fiber gantry
The CO2 laser and the fiber laser each ride on a separate gantry, so the machine cuts two different materials at once. The CO2 laser, 300W, 500W or 600W, cuts acrylic about 1 in. thick, or up to 1.18 in. with the 600W. The 3000W or 6000W fiber laser handles metals, including aluminum and stainless steel. Pick a working area of 5 ft x 10 ft or 6 ft x 12 ft. As an option, the machine comes covered or with laser-control partitions.
- CO2 side: a 300W, 500W or 600W source for non-metals. With compressed air it cuts acrylic about 1 in. thick, or up to 1.18 in. at 600W.
- Fiber side: 3000W or 6000W source for carbon steel, stainless steel, aluminum, brass and copper
- Both gantries run independently and at the same time
- Working area of 5 ft x 10 ft or 6 ft x 12 ft
- Industrial computer loaded with operating and nesting software
- Options: a collector for smells and fumes on the CO2 side, a debris collector on the fiber side
- Enclosed by slide covers or by laser-rated partitions, whichever you choose
- The price covers installation and training. Support comes from Buffalo, Toronto and Kentucky.
Ascent Laser Cutter Configurations
Our 5 ft x 10 ft laser cutters are available in three configurations for different cutting needs.
- CO2 power: 300W, 500W or 600W
- Fiber power: 3000W or 6000W
Dual-gantry, CO2 plus fiber: one gantry cuts nonmetal sheet while the other cuts metal, on the same bed at the same time. It suits shops that switch between many materials.
CO2 only, for nonmetals: clean, precise cuts in acrylic, wood, leather and similar materials.
Fiber only, for metals: fast, accurate cuts in steel, aluminum, brass and other metals.
Laser Cutter Safety Housing Options
Choose from three housing options to suit the machine and your access needs.
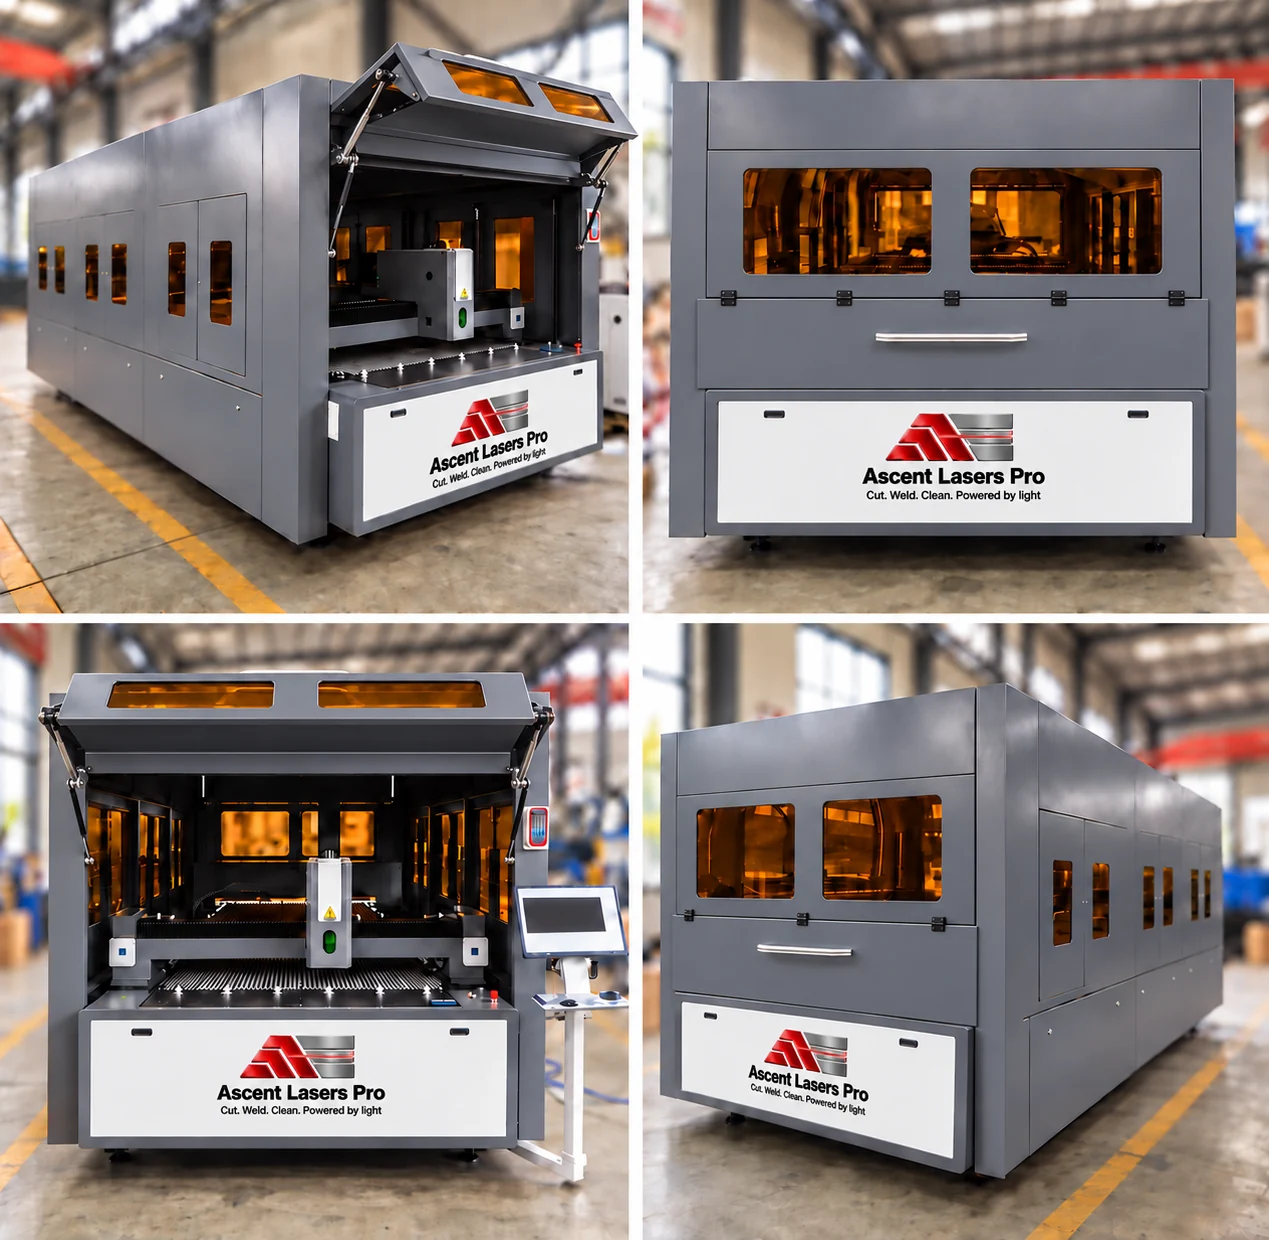
Rigid Cover
A fixed, durable enclosure around the machine.
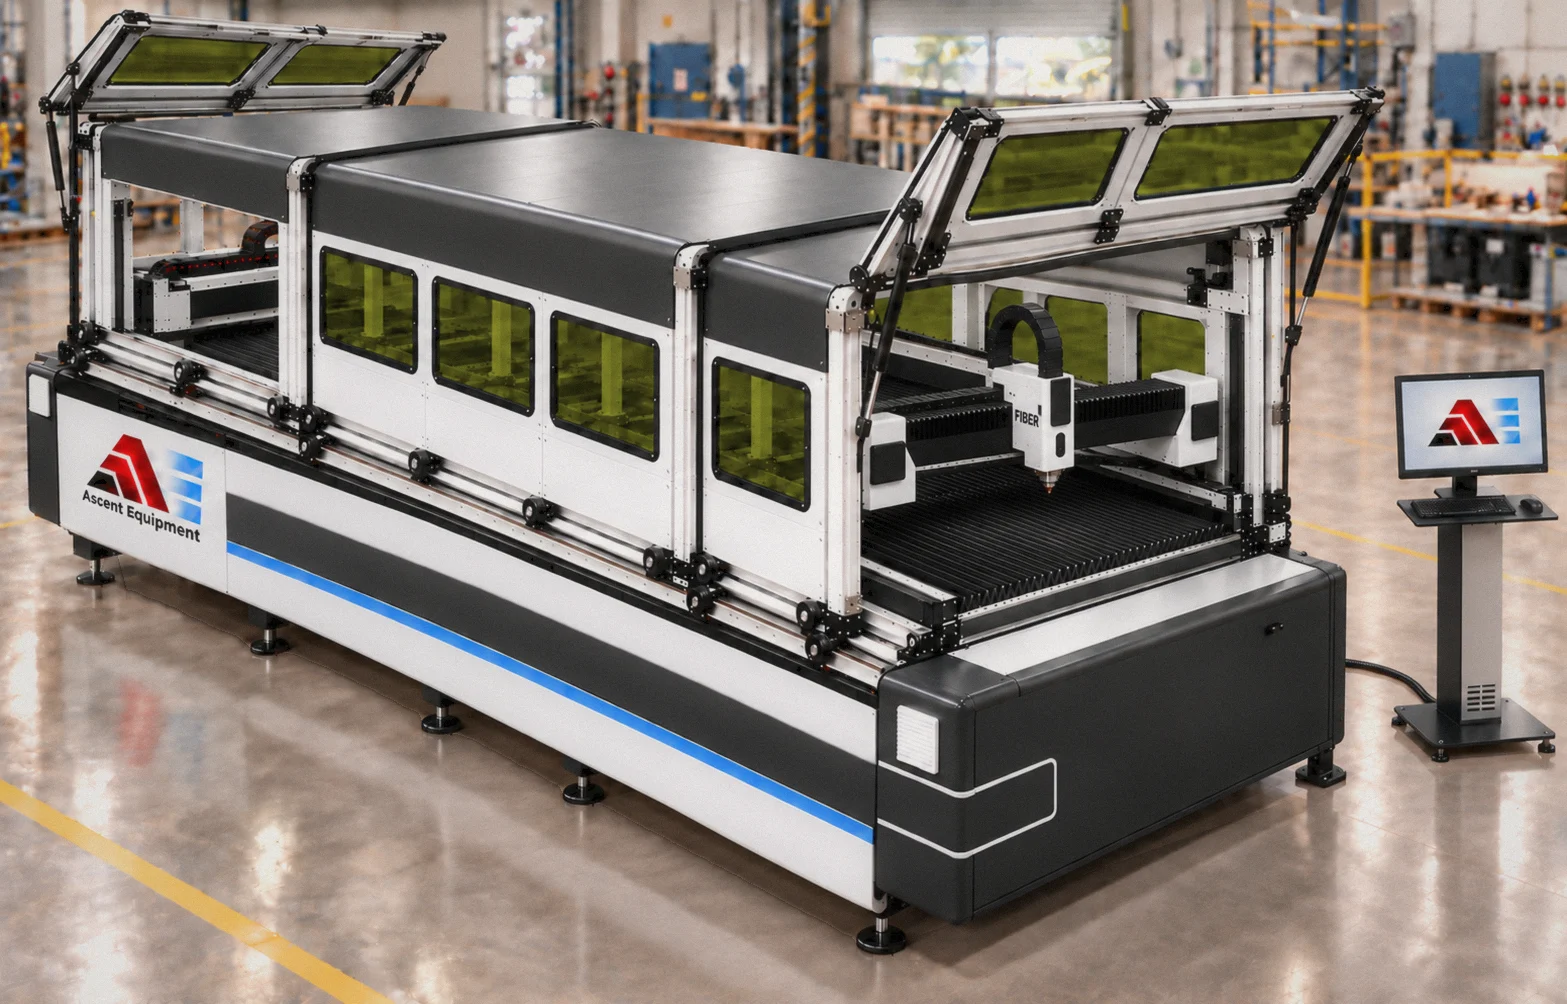
Sliding Covers
Movable covers provide convenient access to the cutting bed.
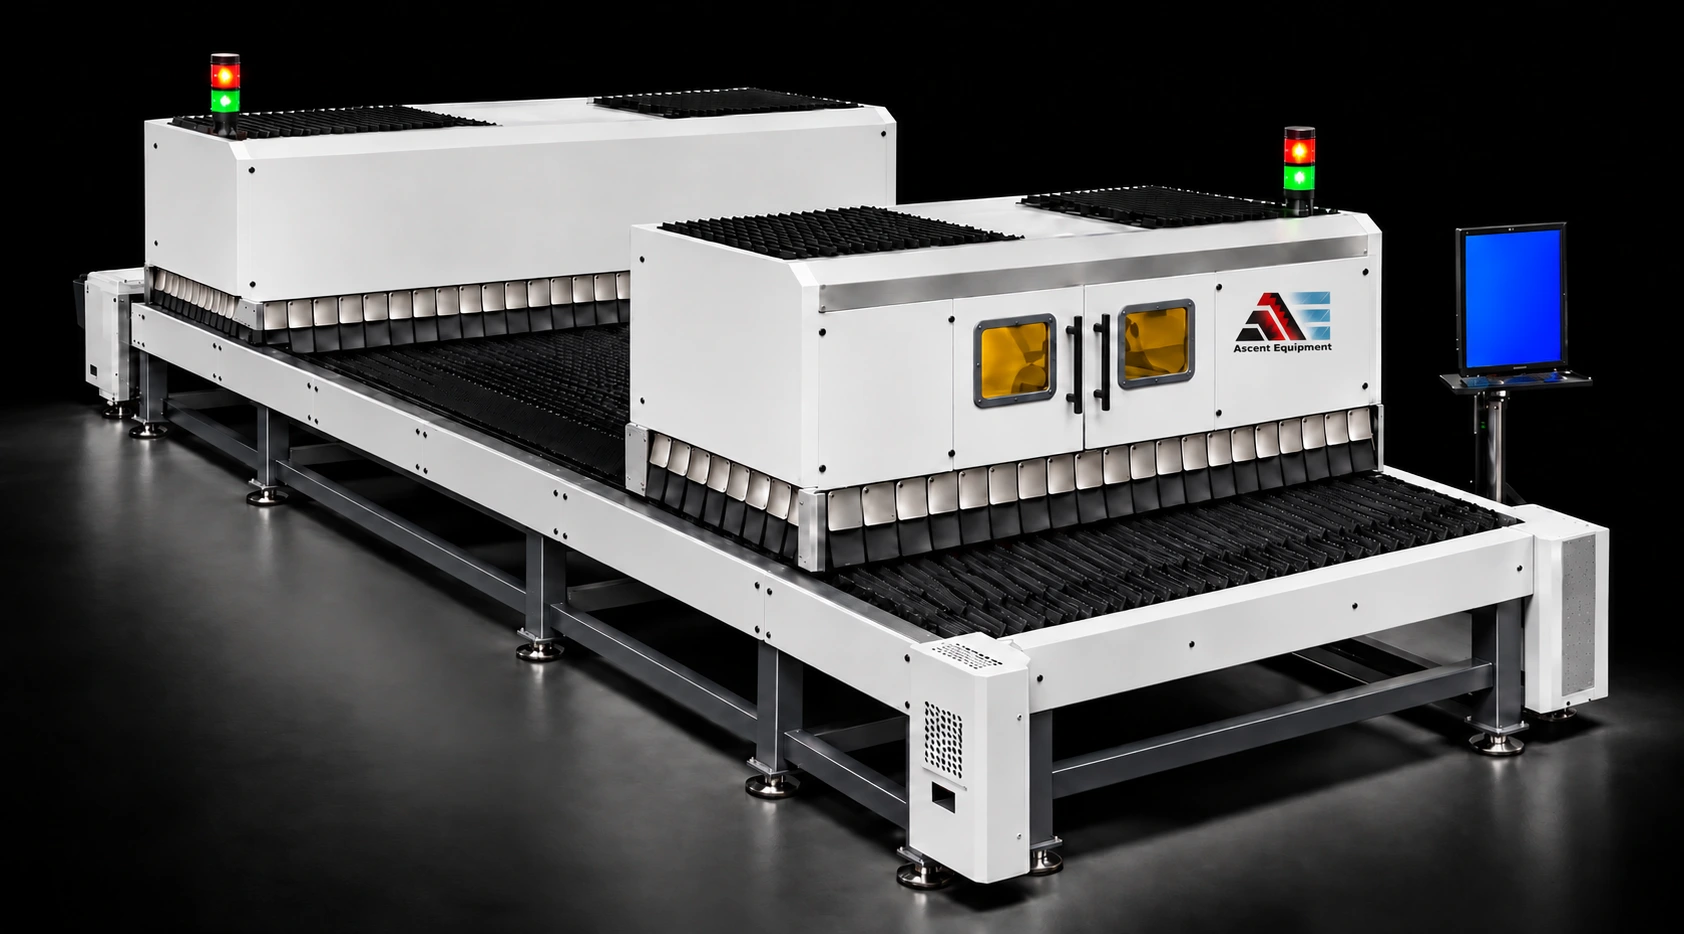
Gantry-Only Covers
Covers around each laser gantry provide protection focused on the gantry area.
Two lasers, two gantries, one table
The dual gantry cutter puts a CO2 laser and a fiber laser on the same machine. Each laser has its own gantry, so the two can work on different materials at the same moment.
- CO2 gantry: a 300W, 500W or 600W laser that cuts acrylic about 1 in. thick, or up to 1.18 in. at 600W.
- Fiber gantry: a 3000W or 6000W laser for metals, among them aluminum and stainless steel
- Working area: 5 ft x 10 ft or 6 ft x 12 ft
- Enclosure option: a cover, or laser-control partitions
Two collectors are offered as further options:
- a collector for the smell and fumes of the CO2 laser
- a collector for the debris of the fiber laser
Installation and training at your shop are part of the price. Our technicians give support from three locations: Buffalo in New York, Toronto in Ontario, and Kentucky.
Free test cut on your material
Send us a sample of your material. We will cut it and report on the cutting speed, at no charge. This way you can judge the quality of the cut and the performance of the machine ahead of a purchase. Contact us to arrange a test.
Watch the machine at work
Cover and partition options
You can have the dual gantry fully covered. The cover adds safety and keeps the noise down.
If you do not order the cover, put the cutter behind laser partitions. You can buy them from us.
Fumes from the cutter should be vented outdoors or passed through a special filter. For more on working safely with lasers, see our laser safety page.
Cutting capacity
CO2 gantry: maximum thickness by material
The table shows the thickest cut the CO2 laser makes in each material, in inches and millimeters, for each tube power.
| Power | Acrylic | MDF | Plywood | Foam | Leather | Wood board |
|---|---|---|---|---|---|---|
| 300W | 0.98 in (25 mm) | 0.59 in (15 mm) | 0.79 in (20 mm) | 1.18 in (30 mm) | 0.31 in (8 mm) | 0.98 in (25 mm) |
| 500W | 0.98 in (25 mm) | 0.59 in (15 mm) | 0.79 in (20 mm) | 1.18 in (30 mm) | 0.31 in (8 mm) | 0.98 in (25 mm) |
| 600W | 1.18 in (30 mm) | 0.79 in (20 mm) | 1.18 in (30 mm) | 1.97 in (50 mm) | 0.39 in (10 mm) | 1.38 in (35 mm) |
Fiber gantry: cutting parameters by metal and thickness
Each table below covers one metal at one laser power. For every thickness it lists the speed, focus position, cut height, gas, nozzle, pressure, power, frequency, duty cycle and cut result.
The cutting gases are liquid oxygen of 99.6% purity and liquid nitrogen of 99.995% purity. Treat these numbers as a reference only. Results change from one customer to the next with gas pressure, nozzles, water cooling, the environment and the way the equipment is configured. A dash marks a value that is not listed.
Row colors: ■ Green is optimal. ■ Yellow means caution, with reduced quality. ■ Red is the maximum thickness, where poor quality is expected.
Fiber laser at 3000W
Carbon steel, Q235B
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | 1,496–1,575 in/min (38–40 m/min) | 0 to -0.02 in (0 to -0.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 1.0 | 12–16 | 3000 | 5000 | 100 | Glossy |
| 0.079 in (2 mm) | — | — | — | — | — | — | — | — | — | — |
| 0.118 in (3 mm) | 157–165 in/min (4–4.2 m/min) | 0.177–0.217 in (4.5–5.5 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.0 | 0.6–0.9 | 3000 | 5000 | 100 | Glossy |
| 0.157 in (4 mm) | 130–138 in/min (3.3–3.5 m/min) | 0.177–0.217 in (4.5–5.5 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.2 | 0.6–0.9 | 3000 | 5000 | 100 | Glossy |
| 0.236 in (6 mm) | 91–98 in/min (2.3–2.5 m/min) | 0.177–0.217 in (4.5–5.5 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.2 | 0.6–0.9 | 3000 | 5000 | 100 | Glossy |
| 0.315 in (8 mm) | 83–87 in/min (2.1–2.2 m/min) | 0.177–0.217 in (4.5–5.5 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.2 | 0.6–0.9 | 3000 | 5000 | 100 | Glossy |
| 0.394 in (10 mm) | 59–67 in/min (1.5–1.7 m/min) | 0.079–0.118 in (2–3 mm) | 0.059 in (1.5 mm) | O2 | Double layer 3.0 | 0.6–0.9 | 2200–2400 | 5000 | 100 | Frosted surface |
| 0.472 in (12 mm) | 47–55 in/min (1.2–1.4 m/min) | 0.079–0.118 in (2–3 mm) | 0.059 in (1.5 mm) | O2 | Double layer 3.0 | 0.6–0.9 | 2200–2400 | 5000 | 100 | Frosted surface |
| 0.551 in (14 mm) | 39–43 in/min (1–1.1 m/min) | 0.079–0.118 in (2–3 mm) | 0.059 in (1.5 mm) | O2 | Double layer 4.0 | 0.6–0.9 | 2200–2400 | 5000 | 100 | Frosted surface |
| 0.63 in (16 mm) | 33–35 in/min (0.85–0.9 m/min) | 0.079–0.118 in (2–3 mm) | 0.059 in (1.5 mm) | O2 | Double layer 4.0 | 0.6–0.9 | 2200–2400 | 5000 | 100 | Frosted surface |
| 0.709 in (18 mm) | 28–30 in/min (0.7–0.75 m/min) | 0.079–0.118 in (2–3 mm) | 0.059 in (1.5 mm) | O2 | Double layer 4.0 | 0.6–0.9 | 2200–2400 | 5000 | 100 | Frosted surface |
| 0.787 in (20 mm) | 24–26 in/min (0.6–0.65 m/min) | 0.079–0.138 in (2–3.5 mm) | 0.059 in (1.5 mm) | O2 | Double layer 4.0 | 0.6–0.9 | 2200–2400 | 5000 | 100 | Frosted surface |
| 0.866 in (22 mm) | 20–22 in/min (0.5–0.55 m/min) | 0.079–0.138 in (2–3.5 mm) | 0.059 in (1.5 mm) | O2 | Double layer 4.0 | 0.6–0.9 | 2200–2400 | 5000 | 100 | Frosted surface |
| 0.984 in (25 mm) | 18–20 in/min (0.45–0.5 m/min) | 0.079–0.138 in (2–3.5 mm) | 0.059 in (1.5 mm) | O2 | Double layer 5.0 | 0.6–0.9 | 2200–2500 | 5000 | 100 | Frosted surface |
Stainless steel, SUS304
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | 1,378–1,457 in/min (35–37 m/min) | 0 to -0.039 in (0 to -1 mm) | 0.02 in (0.5 mm) | N2 | single layer 1.0/1.2/1.5 | 12–16 | 3000 | 5000 | 100 | No residue |
| 0.079 in (2 mm) | 512–591 in/min (13–15 m/min) | -0.059 to -0.079 in (-1.5 to -2 mm) | 0.02 in (0.5 mm) | N2 | single layer 1.5/2.0 | 12–16 | 3000 | 5000 | 100 | No residue |
| 0.118 in (3 mm) | 276–315 in/min (7–8 m/min) | -0.098 to -0.118 in (-2.5 to -3 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0/2.5/3.0 | 16–20 | 3000 | 5000 | 100 | No residue |
| 0.157 in (4 mm) | 177–217 in/min (4.5–5.5 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 | 16–20 | 3000 | 5000 | 100 | No residue |
| 0.236 in (6 mm) | 67–75 in/min (1.7–1.9 m/min) | -0.197 to -0.217 in (-5 to -5.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.5/4.0 | 16–20 | 3000 | 5000 | 100 | No residue |
| 0.315 in (8 mm) | 31–39 in/min (0.8–1.0 m/min) | -0.236 to -0.276 in (-6 to -7 mm) | 0.02 in (0.5 mm) | N2 | single layer 4.0 | 16–20 | 3000 | 5000 | 100 | No residue |
| 0.394 in (10 mm) | 24–28 in/min (0.6–0.7 m/min) | -0.295 to -0.335 in (-7.5 to -8.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 4.0 | 16–20 | 3000 | 5000 | 100 | A small amount of slag |
Aluminum, 6061
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | 1,181–1,299 in/min (30–33 m/min) | -0.02 to -0.039 in (-0.5 to -1 mm) | 0.02 in (0.5 mm) | N2 | single layer 1.0/1.2/1.5 | 12–16 | 3000 | 5000 | 100 | — |
| 0.079 in (2 mm) | 394–472 in/min (10–12 m/min) | -0.039 to -0.059 in (-1 to -1.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 1.5/2.0 | 12–16 | 3000 | 5000 | 100 | — |
| 0.118 in (3 mm) | 217–232 in/min (5.5–5.9 m/min) | -0.098 to -0.118 in (-2.5 to -3 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0/2.5/3.0 | 16–20 | 3000 | 5000 | 100 | — |
| 0.157 in (4 mm) | 110–126 in/min (2.8–3.2 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 | 16–20 | 3000 | 5000 | 100 | — |
| 0.236 in (6 mm) | 28–31 in/min (0.7–0.8 m/min) | -0.197 to -0.217 in (-5 to -5.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.5/4.0 | 16–20 | 3000 | 5000 | 100 | — |
| 0.315 in (8 mm) | 20–24 in/min (0.5–0.6 m/min) | -0.236 to -0.276 in (-6 to -7 mm) | 0.02 in (0.5 mm) | N2 | single layer 4.0 | 16–20 | 3000 | 5000 | 100 | — |
Fiber laser at 6000W
Carbon steel, Q235B
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | 1,811–1,890 in/min (46–48 m/min) | 0 in (0 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | Glossy |
| 0.079 in (2 mm) | 1,378–1,457 in/min (35–37 m/min) | -0.059 in (-1.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | Glossy |
| 0.118 in (3 mm) | 165–177 in/min (4.2–4.5 m/min) | 0.157–0.217 in (4.0–5.5 mm) | 0.024–0.031 in (0.6–0.8 mm) | O2 | Double layer 1.0/1.2 | 0.7–0.9 | 3000–3200 | 5000 | 100 | Glossy |
| 0.157 in (4 mm) | 138–146 in/min (3.5–3.7 m/min) | 0.157–0.217 in (4.0–5.5 mm) | 0.024–0.031 in (0.6–0.8 mm) | O2 | Double layer 1.0/1.2 | 0.7–0.9 | 3900–4200 | 5000 | 100 | Glossy |
| 0.197 in (5 mm) | 126–130 in/min (3.2–3.3 m/min) | 0.157–0.217 in (4.0–5.5 mm) | 0.024–0.031 in (0.6–0.8 mm) | O2 | Double layer 1.0/1.2 | 0.7–0.9 | 4000–4200 | 5000 | 100 | Glossy |
| 0.236 in (6 mm) | 102–110 in/min (2.6–2.8 m/min) | 0.157–0.217 in (4.0–5.5 mm) | 0.024–0.031 in (0.6–0.8 mm) | O2 | Double layer 1.0/1.2 | 0.7–0.9 | 4000–4200 | 5000 | 100 | Glossy |
| 0.315 in (8 mm) | 94–98 in/min (2.4–2.5 m/min) | 0.217–0.256 in (5.5–6.5 mm) | 0.024–0.031 in (0.6–0.8 mm) | O2 | Double layer 1.2 | 0.7–0.9 | 4000–4200 | 5000 | 100 | Glossy |
| 0.394 in (10 mm) | 87–91 in/min (2.2–2.3 m/min) | 0.217–0.256 in (5.5–6.5 mm) | 0.024–0.031 in (0.6–0.8 mm) | O2 | Double layer 1.2 | 0.7–0.9 | 6000 | 5000 | 100 | Glossy |
| 0.472 in (12 mm) | 75–79 in/min (1.9–2.0 m/min) | 0.236–0.276 in (6–7 mm) | 0.024–0.031 in (0.6–0.8 mm) | O2 | Double layer 1.2 | 0.7–0.9 | 6000 | 5000 | 100 | Glossy |
| 0.551 in (14 mm) | 35–39 in/min (0.9–1.0 m/min) | 0.157–0.217 in (4.0–5.5 mm) | 0.024–0.047 in (0.6–1.2 mm) | O2 | Double layer 3.0 | 0.7–0.9 | 2200–2600 | 5000 | 100 | Frosted surface |
| 0.63 in (16 mm) | 31–35 in/min (0.8–0.9 m/min) | 0.118–0.217 in (3.0–5.5 mm) | 0.047–0.059 in (1.2–1.5 mm) | O2 | Double layer 3.0/3.5 | 0.7–0.9 | 2200–2600 | 5000 | 100 | Frosted surface |
| 0.709 in (18 mm) | 28–31 in/min (0.7–0.8 m/min) | 0.118–0.177 in (3.0–4.5 mm) | 0.047–0.059 in (1.2–1.5 mm) | O2 | Double layer 3.5/4.0 | 0.7–0.9 | 2200–2600 | 5000 | 100 | Frosted surface |
| 0.787 in (20 mm) | 24–26 in/min (0.6–0.65 m/min) | 0.079–0.138 in (2–3.5 mm) | 0.047–0.059 in (1.2–1.5 mm) | O2 | Double layer 4.0 | 0.7–0.9 | 2200–2600 | 5000 | 100 | Frosted surface |
| 0.866 in (22 mm) | 22–24 in/min (0.55–0.6 m/min) | 0.079–0.138 in (2–3.5 mm) | 0.047–0.059 in (1.2–1.5 mm) | O2 | Double layer 4.0 | 0.7–0.9 | 2200–2600 | 5000 | 100 | Frosted surface |
| 0.984 in (25 mm) | 20–22 in/min (0.5–0.55 m/min) | 0.079–0.138 in (2–3.5 mm) | 0.047–0.059 in (1.2–1.5 mm) | O2 | Double layer 5.0 | 0.7–0.9 | 2200–2600 | 5000 | 100 | Frosted surface |
Stainless steel, S304
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | 1,772–1,850 in/min (45–47 m/min) | 0 to -0.039 in (0 to -1 mm) | 0.02 in (0.5 mm) | N2 | single layer 1.5 | 12–16 | 6000 | 5000 | 100 | No residue |
| 0.079 in (2 mm) | 1,378–1,457 in/min (35–37 m/min) | -0.059 to -0.079 in (-1.5 to -2 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | No residue |
| 0.118 in (3 mm) | 709–787 in/min (18–20 m/min) | -0.098 to -0.118 in (-2.5 to -3 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | No residue |
| 0.157 in (4 mm) | 551–591 in/min (14–15 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | No residue |
| 0.197 in (5 mm) | 315–394 in/min (8–10 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | No residue |
| 0.236 in (6 mm) | 236–256 in/min (6–6.5 m/min) | -0.197 to -0.217 in (-5 to -5.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 | 12–16 | 6000 | 5000 | 100 | No residue |
| 0.315 in (8 mm) | 157–165 in/min (4–4.2 m/min) | -0.236 to -0.276 in (-6 to -7 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 | 16–20 | 6000 | 5000 | 100 | No residue |
| 0.394 in (10 mm) | 71–79 in/min (1.8–2.0 m/min) | -0.295 to -0.335 in (-7.5 to -8.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 | 16–20 | 6000 | 5000 | 100 | No residue |
| 0.472 in (12 mm) | 43–51 in/min (1.1–1.3 m/min) | -0.295 to -0.335 in (-7.5 to -8.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.5 | 16–20 | 6000 | 5000 | 100 | No residue |
| 0.551 in (14 mm) | 35–39 in/min (0.9–1.0 m/min) | -0.354 to -0.394 in (-9 to -10 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.5 | 16–20 | 6000 | 5000 | 100 | No residue |
| 0.63 in (16 mm) | 31–33 in/min (0.8–0.85 m/min) | -0.394 to -0.433 in (-10 to -11 mm) | 0.02 in (0.5 mm) | N2 | single layer 4.0 | 16–20 | 6000 | 5000 | 100 | A small amount of slag |
| 0.787 in (20 mm) | 20–24 in/min (0.5–0.6 m/min) | -0.433 to -0.512 in (-11 to -13 mm) | 0.02 in (0.5 mm) | N2 | single layer 5.0 | 16–20 | 6000 | 5000 | 100 | A small amount of slag |
Aluminum, 6061
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | 1,969–2,047 in/min (50–52 m/min) | 0 to -0.039 in (0 to -1 mm) | 0.02 in (0.5 mm) | Air | single layer 1.5 | 12–16 | 6000 | 5000 | 100 | — |
| 0.079 in (2 mm) | 1,102–1,142 in/min (28–29 m/min) | -0.059 to -0.079 in (-1.5 to -2 mm) | 0.02 in (0.5 mm) | Air | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | — |
| 0.118 in (3 mm) | 591–669 in/min (15–17 m/min) | -0.098 to -0.118 in (-2.5 to -3 mm) | 0.02 in (0.5 mm) | Air | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | — |
| 0.157 in (4 mm) | 354–394 in/min (9–10 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | Air | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | — |
| 0.197 in (5 mm) | 236–256 in/min (6–6.5 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | Air | single layer 2.5 | 12–16 | 6000 | 5000 | 100 | — |
| 0.236 in (6 mm) | 177–197 in/min (4.5–5 m/min) | -0.197 to -0.217 in (-5 to -5.5 mm) | 0.02 in (0.5 mm) | Air | single layer 2.5 | 12–16 | 6000 | 5000 | 100 | — |
| 0.315 in (8 mm) | 110–114 in/min (2.8–2.9 m/min) | -0.236 to -0.276 in (-6 to -7 mm) | 0.02 in (0.5 mm) | Air | single layer 2.5 or 3.0 | 16–20 | 6000 | 5000 | 100 | — |
| 0.394 in (10 mm) | 75–79 in/min (1.9–2 m/min) | -0.295 to -0.335 in (-7.5 to -8.5 mm) | 0.02 in (0.5 mm) | Air | single layer 3.0 or 3.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.472 in (12 mm) | 43–47 in/min (1.1–1.2 m/min) | -0.295 to -0.335 in (-7.5 to -8.5 mm) | 0.02 in (0.5 mm) | Air | single layer 3.0 or 3.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.551 in (14 mm) | 31–39 in/min (0.8–1.0 m/min) | -0.354 to -0.394 in (-9 to -10 mm) | 0.02 in (0.5 mm) | Air | single layer 3.0 or 3.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.63 in (16 mm) | 20–24 in/min (0.5–0.6 m/min) | -0.354 to -0.394 in (-9 to -10 mm) | 0.02 in (0.5 mm) | Air | single layer 4.0 | 16–20 | 6000 | 5000 | 100 | — |
Brass
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | 1,772–2,165 in/min (45–55 m/min) | 0 to -0.039 in (0 to -1 mm) | 0.02 in (0.5 mm) | N2 | single layer 1.5 | 12–16 | 6000 | 5000 | 100 | — |
| 0.079 in (2 mm) | 984–1,378 in/min (25–35 m/min) | -0.059 to -0.079 in (-1.5 to -2 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 12–16 | 6000 | 5000 | 100 | — |
| 0.118 in (3 mm) | 669–787 in/min (17–20 m/min) | -0.098 to -0.118 in (-2.5 to -3 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 16–20 | 6000 | 5000 | 100 | — |
| 0.157 in (4 mm) | 394–472 in/min (10–12 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.0 | 16–20 | 6000 | 5000 | 100 | — |
| 0.197 in (5 mm) | 276–315 in/min (7–8 m/min) | -0.138 to -0.157 in (-3.5 to -4 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.236 in (6 mm) | 197–236 in/min (5–6 m/min) | -0.197 to -0.217 in (-5 to -5.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.315 in (8 mm) | 79–118 in/min (2–3 m/min) | -0.236 to -0.276 in (-6 to -7 mm) | 0.02 in (0.5 mm) | N2 | single layer 2.5 or 3.0 | 16–20 | 6000 | 5000 | 100 | — |
| 0.394 in (10 mm) | 63–79 in/min (1.6–2 m/min) | -0.295 to -0.335 in (-7.5 to -8.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 or 3.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.472 in (12 mm) | 51–67 in/min (1.3–1.7 m/min) | -0.295 to -0.335 in (-7.5 to -8.5 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 or 3.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.551 in (14 mm) | 31–39 in/min (0.8–1.0 m/min) | -0.354 to -0.394 in (-9 to -10 mm) | 0.02 in (0.5 mm) | N2 | single layer 3.0 or 3.5 | 16–20 | 6000 | 5000 | 100 | — |
| 0.63 in (16 mm) | 20–24 in/min (0.5–0.6 m/min) | -0.354 to -0.394 in (-9 to -10 mm) | 0.02 in (0.5 mm) | N2 | single layer 4.0 | 16–20 | 6000 | 5000 | 100 | — |
Fiber laser at 12000W (fiber-only machine)
These 12000W settings are for a fiber-only machine. The dual gantry is built with a 3000W or 6000W fiber laser.
Stainless steel, SUS304
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | — | — | — | N2 | Single layer 1.5 | — | — | 5000 | 100 | — |
| 0.236 in (6 mm) | 630 in/min (16 m/min) | -0.098 to -0.118 in (-2.5 to -3 mm) | 0.02 in (0.5 mm) | N2 | Single layer 3.0 | 12–14 | 12000 | 5000 | 100 | — |
| 0.315 in (8 mm) | 394 in/min (10 m/min) | -0.118 to -0.157 in (-3 to -4 mm) | 0.02 in (0.5 mm) | N2 | Single layer 3.5 | 14–16 | 12000 | 5000 | 100 | — |
| 0.394 in (10 mm) | 236 in/min (6 m/min) | -0.236 to -0.256 in (-6 to -6.5 mm) | 0.02 in (0.5 mm) | N2 | Single layer 4.0 | 14–16 | 12000 | 5000 | 100 | — |
| 0.472 in (12 mm) | 157 in/min (4 m/min) | -0.276 to -0.295 in (-7 to -7.5 mm) | 0.02 in (0.5 mm) | N2 | Single layer 4.0 | 14–16 | 12000 | 5000 | 100 | — |
| 0.551 in (14 mm) | 138 in/min (3.5 m/min) | -0.354 to -0.394 in (-9 to -10 mm) | 0.02 in (0.5 mm) | N2 | Single layer 4.0 | 14–16 | 12000 | 5000 | 100 | — |
| 0.63 in (16 mm) | 102 in/min (2.6 m/min) | -0.433 to -0.472 in (-11 to -12 mm) | 0.02 in (0.5 mm) | N2 | Single layer 5.0 | 14–16 | 12000 | 5000 | 100 | — |
| 0.709 in (18 mm) | 79 in/min (2 m/min) | -0.551 to -0.591 in (-14 to -15 mm) | 0.02 in (0.5 mm) | N2 | Single layer 5.0 | 14–16 | 12000 | 5000 | 100 | — |
| 0.787 in (20 mm) | 63 in/min (1.6 m/min) | -0.591 to -0.61 in (-15 to -15.5 mm) | 0.02 in (0.5 mm) | N2 | Single layer 5.0 | 16–18 | 12000 | 5000 | 100 | — |
| 0.984 in (25 mm) | 39 in/min (1 m/min) | -0.709 to -0.748 in (-18 to -19 mm) | 0.02 in (0.5 mm) | N2 | Single layer 5.0 | 18–20 | 12000 | 5000 | 100 | — |
| 1.181 in (30 mm) | 20 in/min (0.5 m/min) | 0.276 in (7 mm) | 0.02 in (0.5 mm) | N2 | Single layer 5.0 | 18–20 | 12000 | 5000 | 100 | — |
| 1.575 in (40 mm) | 8 in/min (0.2 m/min) | 0.276 in (7 mm) | 0.02 in (0.5 mm) | N2 | Single layer 5.0 | 18–20 | 12000 | 200 | 100 | — |
| 1.969 in (50 mm) | 5 in/min (0.12 m/min) | 0.276 in (7 mm) | 0.02 in (0.5 mm) | N2 | Single layer 5.0 | 18–20 | 12000 | 200 | 100 | — |
Carbon steel, Q235
| Thickness | Speed | Focus position | Cut height | Gas | Nozzle | Pressure bar | Power W | Frequency Hz | Duty cycle % | Cut result |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.039 in (1 mm) | — | — | — | N2 | Single layer 1.5 | — | — | 5000 | 100 | — |
| 0.157 in (4 mm) | 130–138 in/min (3.3–3.5 m/min) | 0.276–0.315 in (7–8 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.0/1.2 | 0.6–0.8 | 3000–3200 | 5000 | 100 | — |
| 0.236 in (6 mm) | 106–114 in/min (2.7–2.9 m/min) | 0.315–0.354 in (8–9 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.0/1.2 | 0.6–0.8 | 3900–4200 | 5000 | 100 | — |
| 0.315 in (8 mm) | 94–98 in/min (2.4–2.5 m/min) | 0.335–0.394 in (8.5–10 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.2 | 0.6–0.8 | 3900–4200 | 5000 | 100 | — |
| 0.394 in (10 mm) | 79–83 in/min (2.0–2.1 m/min) | 0.354–0.394 in (9–10 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.2 | 0.6–0.8 | 4200–4500 | 5000 | 100 | — |
| 0.472 in (12 mm) | 75–79 in/min (1.9–2 m/min) | 0.354–0.394 in (9–10 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.2 | 0.6–0.8 | 6000–7000 | 5000 | 100 | — |
| 0.551 in (14 mm) | 67–71 in/min (1.7–1.8 m/min) | 0.374–0.413 in (9.5–10.5 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.2 | 0.6–0.8 | 7000–8000 | 5000 | 100 | — |
| 0.63 in (16 mm) | 61–63 in/min (1.55–1.6 m/min) | 0.394–0.433 in (10–11 mm) | 0.039 in (1 mm) | O2 | Double layer 1.4 | 0.6–0.8 | 8000-9000 | 5000 | 100 | — |
| 0.709 in (18 mm) | 53–55 in/min (1.35–1.4 m/min) | 0.394–0.433 in (10–11 mm) | 0.039 in (1 mm) | O2 | Double layer 1.4 | 0.6–0.8 | 10000 | 5000 | 100 | — |
| 0.787 in (20 mm) | 47–51 in/min (1.2–1.3 m/min) | 0.433–0.472 in (11–12 mm) | 0.031 in (0.8 mm) | O2 | Double layer 1.6 | 0.8–1 | 10000 | 5000 | 100 | — |
| 0.866 in (22 mm) | 31–35 in/min (0.8–0.9 m/min) | 0.433–0.472 in (11–12 mm) | 0.028 in (0.7 mm) | O2 | Double layer 1.6 | 1 | 12000 | 5000 | 100 | — |
| 0.984 in (25 mm) | 24–28 in/min (0.6–0.7 m/min) | 0.512–0.551 in (13–14 mm) | 0.024 in (0.6 mm) | O2 | Double layer 1.8 | 1.2 | 12000 | 5000 | 100 | — |
| 1.181 in (30 mm) | 14–18 in/min (0.35–0.45 m/min) | 0.512–0.551 in (13–14 mm) | 0.024 in (0.6 mm) | O2 | Double layer 1.8 | 1.2 | 12000 | 5000 | 100 | — |
| 1.378 in (35 mm) | 14–16 in/min (0.35–0.4 m/min) | 0.512–0.551 in (13–14 mm) | 0.024 in (0.6 mm) | O2 | Double layer 1.8 | 1.3 | 12000 | 5000 | 100 | — |
| 1.575 in (40 mm) | 12–14 in/min (0.3–0.35 m/min) | 0.512–0.551 in (13–14 mm) | 0.047 in (1.2 mm) | O2 | Double layer 1.8 | 1.2–1.6 | 12000 | 5000 | 100 | — |
| 1.772 in (45 mm) | 8–10 in/min (0.2–0.25 m/min) | 0.512–0.551 in (13–14 mm) | 0.047 in (1.2 mm) | O2 | Double layer 1.8 | 1.2–1.6 | 12000 | 5000 | 100 | — |
Machine components
The dual gantry includes the following.
| Item | Specification |
|---|---|
| CO2 laser power | 300W, 500W or 600W |
| Fiber laser power | 3000W or 6000W |
| CO2 laser tube | 300W, 500W or 600W |
| CO2 laser controller | Separate controller for the CO2 gantry |
| Cutting head and controller | Fiber cutting head and controller, with remote DSP panel |
| Laser head | Autofocus |
| CCD camera | Large, optional |
| Z axis transmission | Ball screw |
| X and Y axis transmission | Helical rack and pinion |
| Y axis drive | Dual driver |
| Reducer | MOTO |
| Guide rails | LAPPING, 25 mm (0.98") |
| Servo motor and drivers | 750W |
| Pneumatic elements | Industrial grade |
| Water chillers | 2 |
| Computer | Industrial, with Wi-Fi |
| Air compressor for the CO2 laser | Oil-free |
| Electrical supply | 380V 3-phase and 220V 1-phase, 60Hz. Give us your shop's three-phase voltage, and we can provide a matching transformer for 380V. |
The photo below shows two CO2 laser tubes, a 500W and a 300W.
Control software
One industrial computer runs both gantries. It comes with operating and nesting software, with one control program for the CO2 gantry and one for the fiber gantry.
Both programs are included with the machine. The cutter takes standard DXF files, which you can export from almost any graphics or CAD program, so no proprietary file format locks you in.
Consumables
- Cutting nozzles: 10 pcs
- Protection lenses: 5 pcs
- Ceramic rings: 2 pcs
Warranty and support
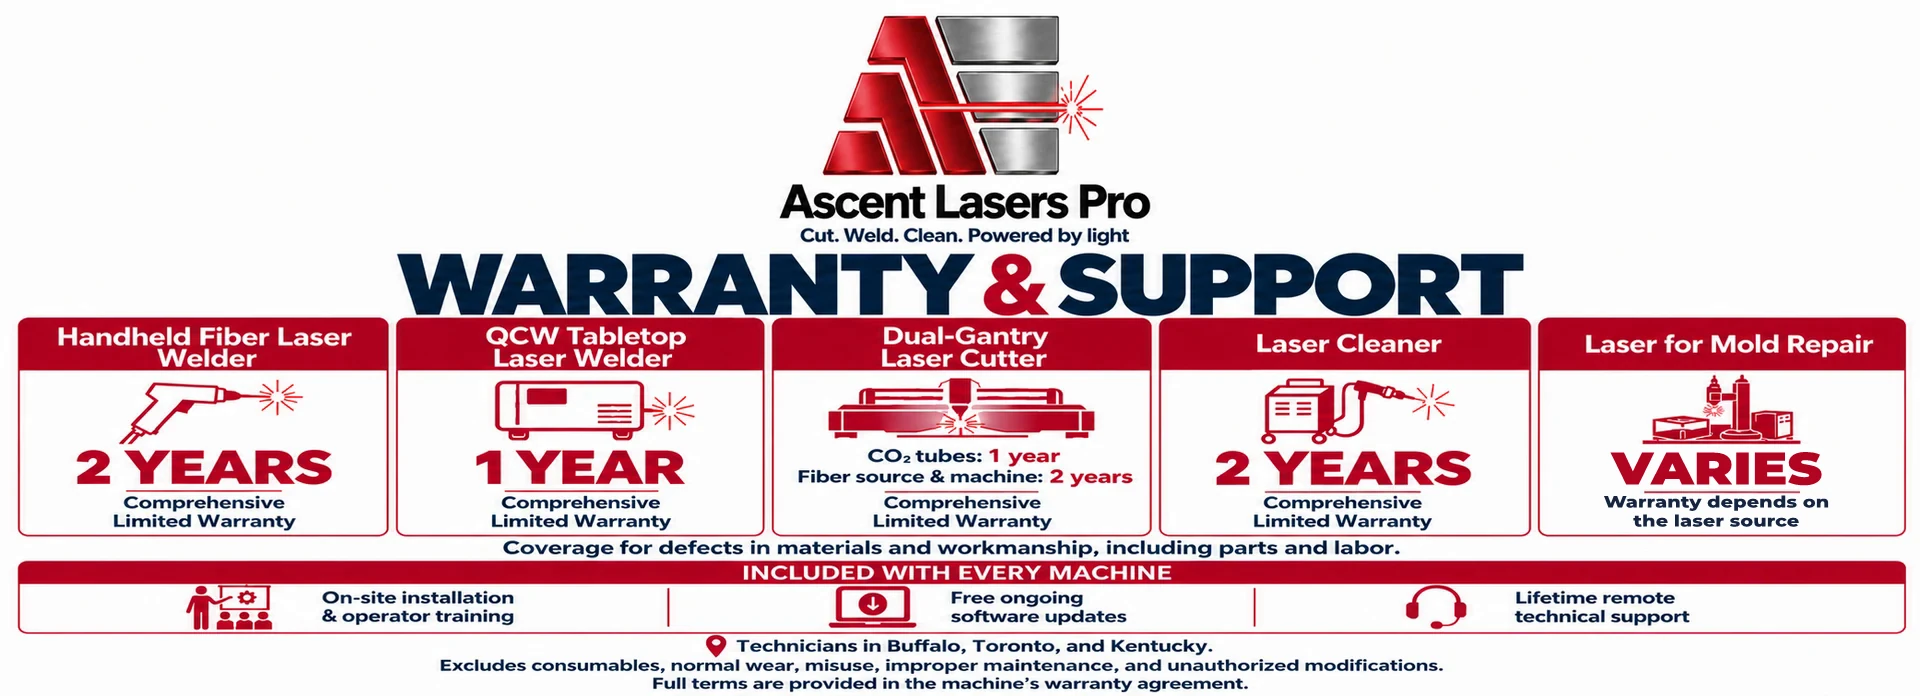
- Fiber laser source: 2 years
- All other non-consumable components: 2 years
- CO2 laser source: 1 year. A CO2 tube wears with use, and its typical service life is 12,000 hours.
The quoted price has no add-ons or hidden fees. Shipping and on-site installation and training are included in the price. Software updates cost nothing, and remote diagnostics and assistance continue for the life of the machine. Remote desktop software is pre-installed, so a technician can respond quickly with remote help or retraining.
CO2 or fiber: which laser for which material
| Application | CO2 laser | Fiber laser |
|---|---|---|
| Acrylic cutting | Excellent | Not recommended |
| Wood / MDF | Excellent | No |
| Engraving | Excellent | Good on metal |
| Stainless steel | Limited | Excellent |
| Aluminum cutting | Limited | Excellent |
The dual gantry gives you both lasers in one machine. The two gantries are independent, and each does its own job at the same time over the same table.
Read next