Fiber laser cutters have taken over a large share of metal cutting from plasma, mechanical cutting and older CO₂ lasers. They cut quickly, hold tight tolerances and need little upkeep. This article explains why shops are making the switch and what to look for in a machine.
How a fiber laser cuts metal
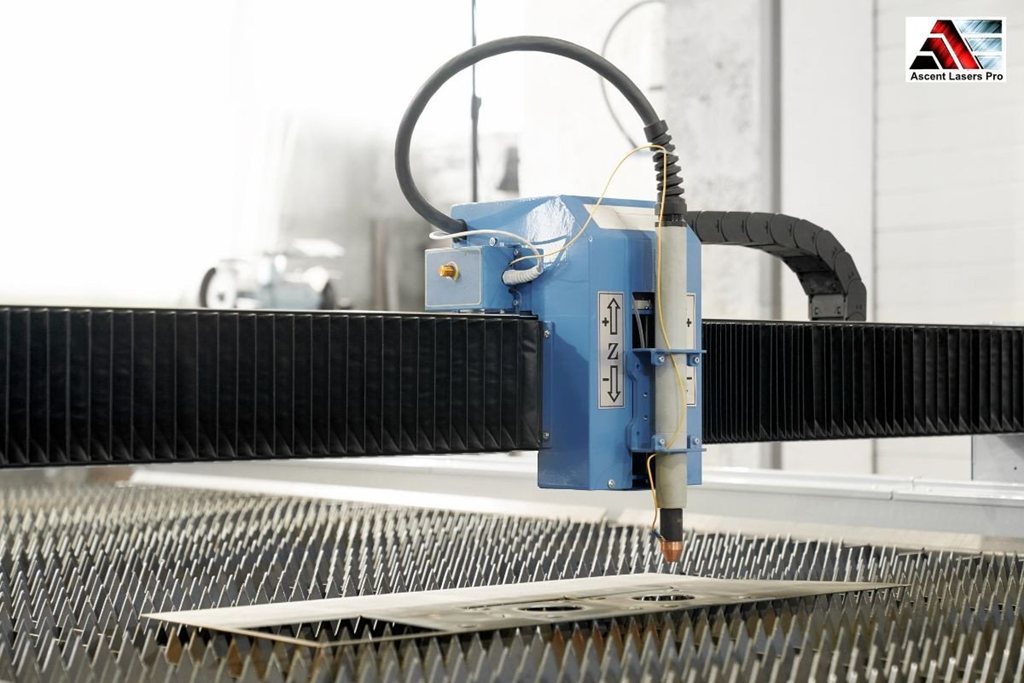
A fiber laser creates its beam in a fiber optic cable and delivers it to a cutting head. The head focuses the beam into a tiny spot, which melts the metal along the cutting path while a stream of assist gas blows the molten material out of the cut. The result is a narrow, accurate cut, and it works on a wide range of metals.
Advantages of fiber laser cutting
Speed
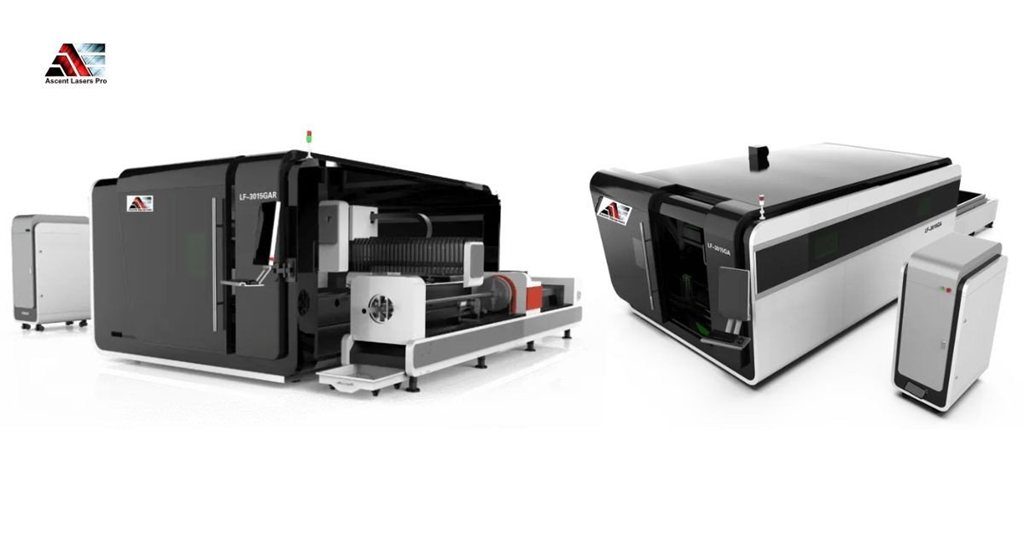
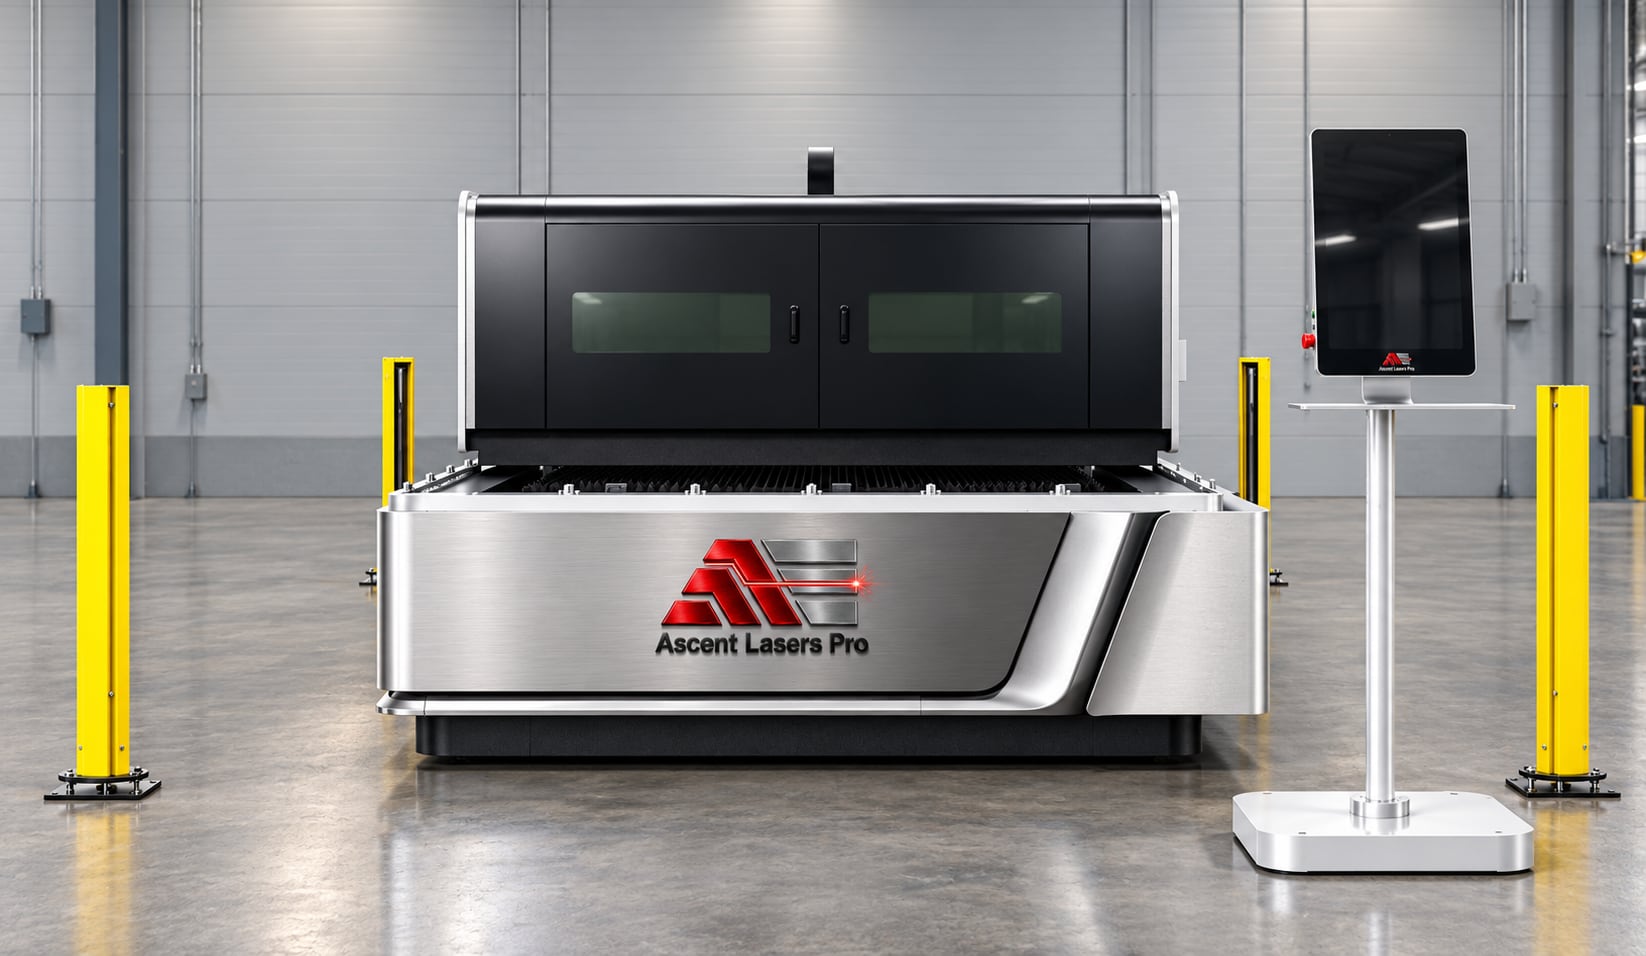
A fiber laser puts its energy into a very small area, so it cuts fast, especially on thin and medium sheet. Faster cutting cuts production time. The Ascent A-C Series fiber laser cutter has a maximum linkage speed of 180 m/min (590 ft/min), and its exchange table lets the operator load the next sheet outside the enclosure.
Precision
Accuracy matters when a small error can ruin a part. The Ascent cutters list a positioning accuracy of ±0.05 mm/m (±0.00197 in/m) and a repositioning accuracy of ±0.03 mm (±0.00118 in). Laser cuts are clean and often burr-free, which means less finishing.
Range of metals
A fiber laser handles carbon steel, stainless steel, aluminum and brass, and the cutting tables on the Ascent page show speeds by thickness at each power level. For example, the reference figure for stable cutting in carbon steel is 16 mm (0.63 in) at 3 kW and 25 mm (0.98 in) at 6 kW. The Ascent dual gantry cutter also lists copper.
Low maintenance
A fiber laser source is solid state, with no laser tube or flash lamp to replace. The machine still needs routine care: keep the cutting head optics clean, replace nozzles and protective lenses, and look after the water chiller.
Energy efficiency
Fiber lasers use electricity more efficiently than CO₂ lasers, so they cost less to run for the same cutting job.
Less waste
A narrow beam makes a narrow cut, so you can nest parts closely and lose less material. The heat-affected zone is small, which keeps the area around the cut in better condition.
Where fiber laser cutters are used
- Automotive. Body parts, frames and custom components.
- Aerospace. Thin-walled parts with tight tolerances.
- Medical. Small, intricate parts.
- Fabrication and custom work. Brackets, enclosures, panels and one-off parts.
Smaller workshops use fiber lasers for custom jobs too, because the machine handles many designs and materials with a change of file and settings.
Automation
Many shops add loading and unloading equipment or robotic handling to a fiber laser. The exchange table on the Ascent A-C Series is a first step in that direction, and a sheet loading module is an option.
Safety
A fiber laser cutter is a Class 4 laser. Guard the work area, vent fumes, and follow the guidance on our laser safety page. The Ascent A-C and A-I Series are fully enclosed, the A-A Series has a gantry cover and safety light curtains, and Ascent laser complies with applicable FDA laser product requirements.
Choosing a fiber laser cutter
Match the power to the metals and thicknesses you cut. Look at accuracy, speed, software, enclosure, cooling and support. The Ascent cutters come with the laser source, laser head, control system and water chiller. Shipping, installation and training at your facility are included in the price, and the warranty is 5 years on the laser head, laser source and control system, and 3 years on the entire system.
As output grows, loading sheets by hand often becomes the slow step. Sheet Loading for Laser Cutters compares the options and what they cost.
For help, visit Ascent Lasers Pro or contact us.